RBM Boiler Water Treatment Chemical About
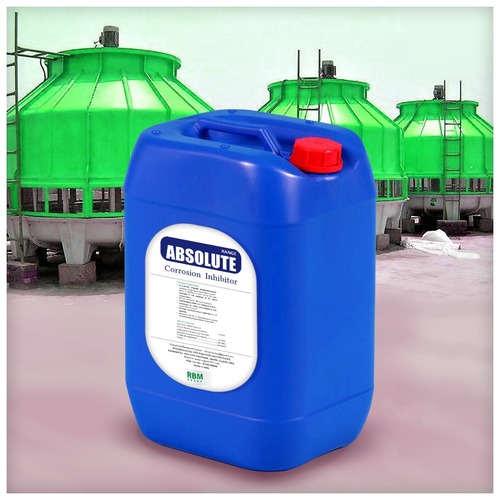
Experience triumphant results with RBM Boiler Water Treatment Chemical-an excellent choice for industrial boiler systems. This high-purity, technical-grade liquid blend is formulated to prevent scale and corrosion, maintaining commanding system efficiency. Packaging is in durable 25 kg blue cans, with a recommended concentration as per industry guidelines. Engineered for complete solubility and easy application, this clear liquid chemical boasts a mild scent and is non-poisonous. Personalise your treatment process with RBM's specialty formulation, trusted by favorable reviews across dealers, distributors, and industrial users nationwide. Purchase with confidence from leading suppliers, retailers, and exporters across India.
Comprehensive Solution with Distinct Features
RBM Boiler Water Treatment Chemical stands out with its specialty formulation, which is engineered specifically for boilers. Its main features include high purity, stable alkaline pH, and a clear, completely water-soluble liquid form. This product's primary competitive advantage is its effective prevention of both scaling and corrosion, ensuring long-term system integrity. Dependable packaging, reliable shelf life of 12 months, and user-friendly application further elevate its position as a preferred choice among industrial boiler operators.
Sample Policy & Certifications for Confidence
RBM provides samples for evaluation on proposal amount payment, ensuring suitability before large-scale order completion. Upon finalizing the order, samples are dispatched promptly to aid in informed decision-making. Our chemical is backed by relevant quality certifications, verifying its performance and compliance. This clear approach enhances trust during the procurement process and supports industrial buyers nationwide. RBM's commitment to quality and transparency positions us as a trustworthy partner for all boiler water treatment needs.
FAQ's of RBM Boiler Water Treatment Chemical:
Q: How should the RBM Boiler Water Treatment Chemical be used in industrial applications?
A: Follow the recommended concentration guidelines provided on the label or technical data sheet to ensure optimal results. Add the liquid directly to the boiler system, ensuring complete solubility and uniform mixing for maximum effectiveness.
Q: What are the main benefits of using RBM Boiler Water Treatment Chemical?
A: This product prevents scale buildup and corrosion within industrial boilers, which helps prolong equipment life, improve operational efficiency, and reduce maintenance costs over time.
Q: Where can I purchase RBM Boiler Water Treatment Chemical in India?
A: This product is available through leading dealers, distributors, retailers, suppliers, and exporters throughout India, ensuring easy accessibility across major industrial regions.
Q: What makes the RBM Boiler Water Treatment Chemical a competitive choice?
A: Its specialty boiler-friendly formulation, high purity, excellent solubility, and user-safe alkaline nature make it a commanding, excellent solution backed by favorable reviews and trusted by various industry professionals.
Q: When is the best time to replace or replenish the boiler chemical?
A: Replenishment should be aligned with your routine boiler maintenance cycle or as indicated by water quality monitoring. Always adhere to the shelf life of 12 months and store the container in a cool, dry place for best results.
Q: What process is followed for requesting and dispatching a sample?
A: After submitting a proposal amount, samples are promptly dispatched to facilitate evaluation prior to order completion. This policy ensures you can assess product suitability for your specific boiler system.
 Mon-Sat 9.00 AM to 6.00 PM


 Send Inquiry




 Send Inquiry

 Send Inquiry
 Send SMS
 Call Me Free


 English
 Spanish
 French
 German
 Italian
 Chinese (Simplified)
 Japanese
 Korean
 Arabic
 Portuguese
